Custom CNC Turned Aluminum Ring Flanges
Product Overview:
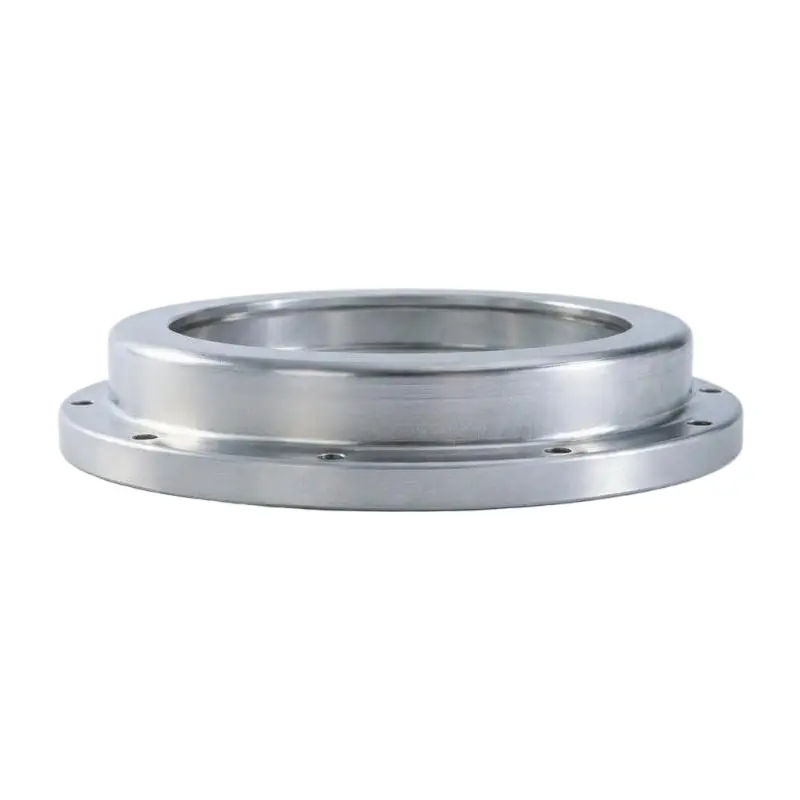
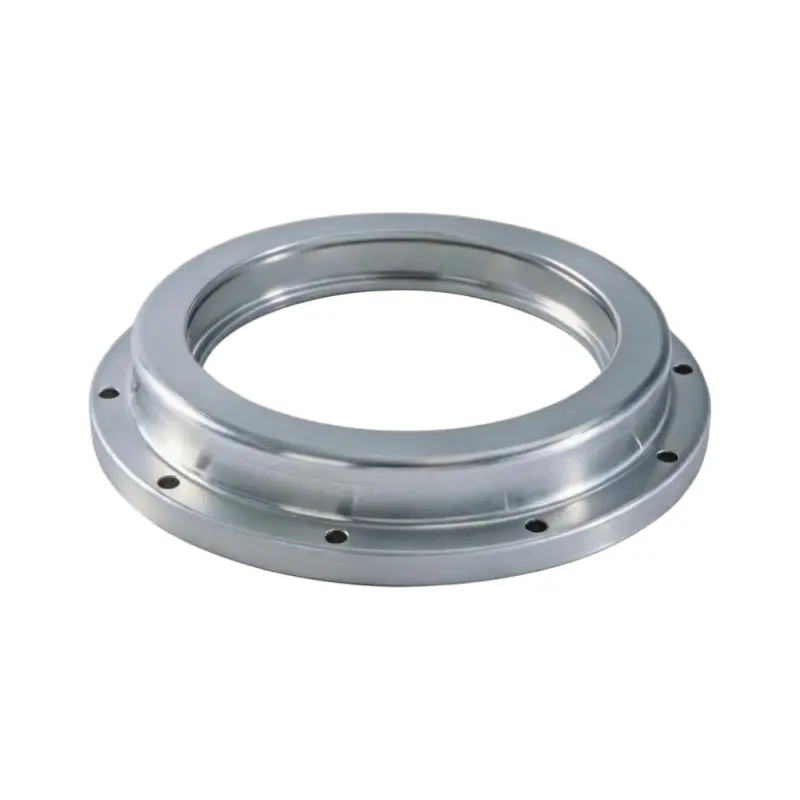
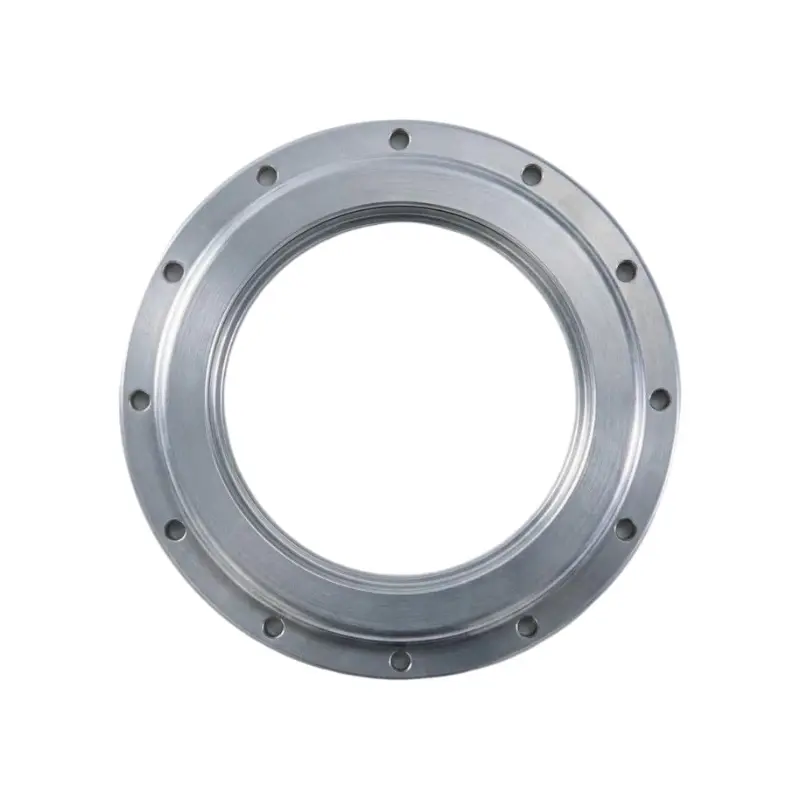
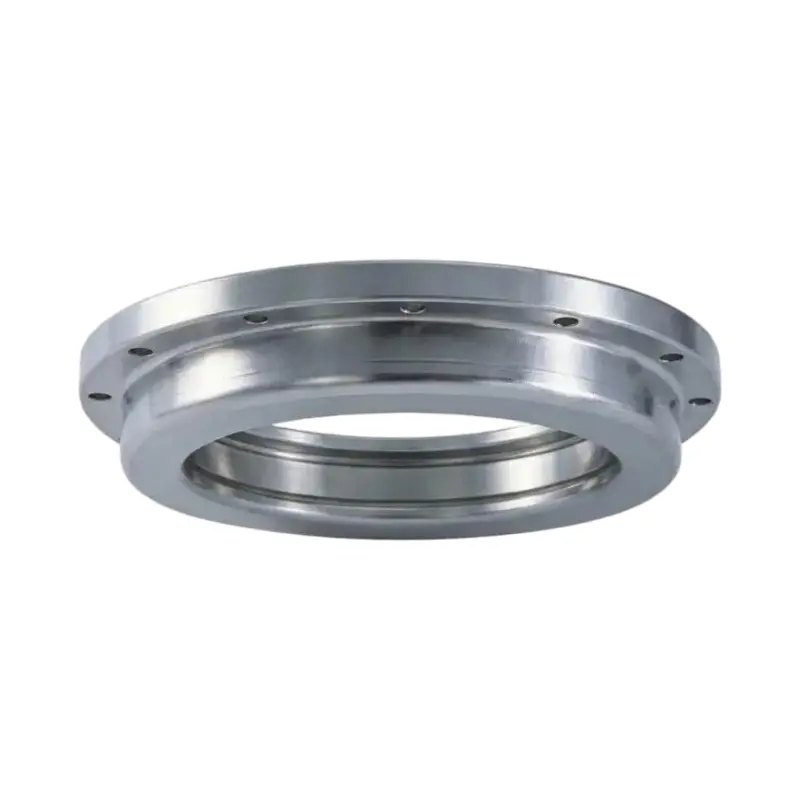
FlexiTurn custom CNC machines aluminum ring flanges from 6061-T6 and 7075-T6 billets to your 2D/3D CAD data. We machine stepped bores, pilot outer diameters, flange faces, and bolt-hole patterns with unified datum control, then coordinate anodizing with pre-machining dimensional compensation to preserve final fit. Prototype to production supported.
Workmanship: CNC Turning, CNC Drilling, 4 Axis CNC Machining, 3 Axis CNC Machining
Material: Aluminum
Inquiry Email: sales@flexiturn.com
Custom CNC Turned Aluminum Ring Flanges Details
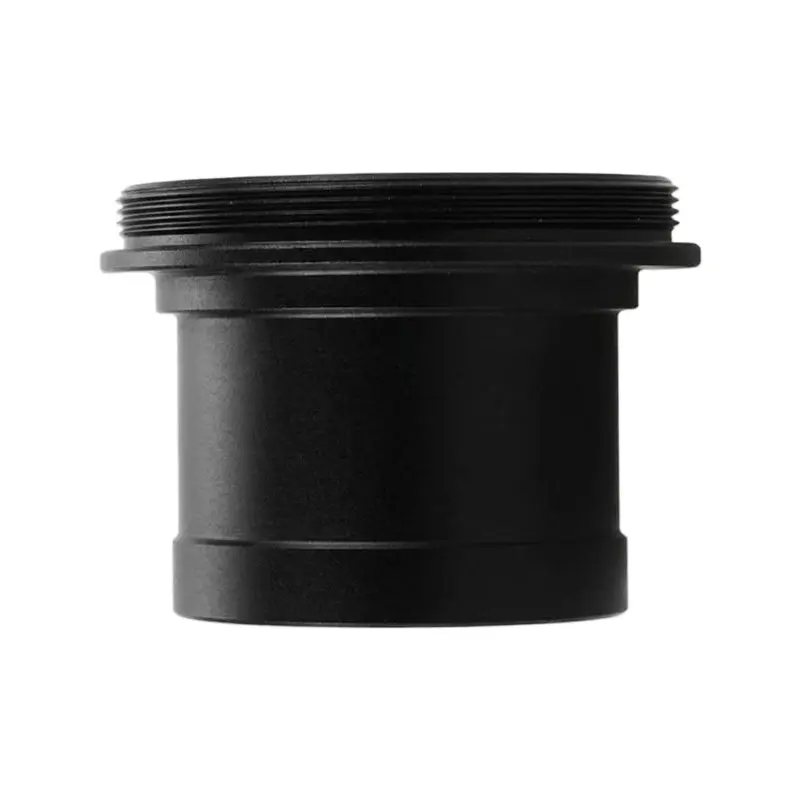
FlexiTurn provides precision CNC turning services for custom aluminum ring flanges, exemplified by the spigot flange shown above. This part features a central stepped bore, a precision pilot outer diameter (locating spigot), an outer bolt circle, and a machined mounting face. Every dimension and geometric tolerance is defined by your 2D or 3D CAD data. FlexiTurn is a CNC machining service provider — the flange you receive is machined to your drawing.
The service FlexiTurn delivers is the controlled turning and secondary machining process: converting your design into a functional aluminum ring flange with defined bore geometry, pilot diameter precision, bolt-hole position, and face condition.
Machining Capabilities
A spigot ring flange appears straightforward until two functional requirements interact: the pilot diameter that centers the part in a mating bore, and the bolt circle that clamps the flange down. If these features are machined in separate setups without a unified datum, bolt tightening will distort the alignment. FlexiTurn addresses this with the following process controls:
Unified-Datum CNC Turning: Coaxial features — stepped bore, pilot outer diameter, and flange faces — are machined relative to a common primary datum in a single setup. This supports critical concentricity between the inner bore and outer pilot diameter.
Indexed Bolt-Hole Machining: Bolt holes are machined using C-axis indexing on the lathe or a 4-axis milling center, rather than re-chucking for each hole. This controls angular spacing and true position of the bolt pattern relative to the central bore.
Stepped Bore & Spigot Control: The stepped bore and outer pilot are machined with separate rough and finish passes to control roundness, diameter tolerance, and surface finish across bearing seats and locating shoulders.
Face Runout and Flatness Control: The mounting face is finished to controlled flatness and runout, supporting even clamp load and preventing cocking under bolt torque.
Material Selection
FlexiTurn machines aluminum ring flanges from the alloys most commonly specified for structural and rotating interfaces:
6061-T6: Good machinability, moderate strength, and consistent anodizing response. Suitable for general automation mounts, sensor bases, and non-load-critical rotating interfaces.
7075-T6: Higher strength-to-weight ratio than 6061. Suitable for servo motor mounts, drive flanges, and weight-sensitive rotating assemblies.
Both grades are sourced from certified suppliers with documented mill test reports.
Tolerances & Quality
Typical machining capabilities for aluminum ring flanges:
Bore and pilot diameter concentricity: ≤0.02 mm TIR, relative to central datum bore, for features ≤100 mm nominal diameter
Bolt-hole true position: within ⌀0.02–0.03 mm relative to the central bore, verified on critical patterns
Flange face runout: ≤0.01 mm TIR for rotating interfaces; tighter available upon engineering review
Mating face roughness: Ra 1.6–3.2 μm as-turned; Ra 0.8 μm or finer available with finish operations
General tolerances: ISO 2768-m, or ±0.05 mm on non-critical features
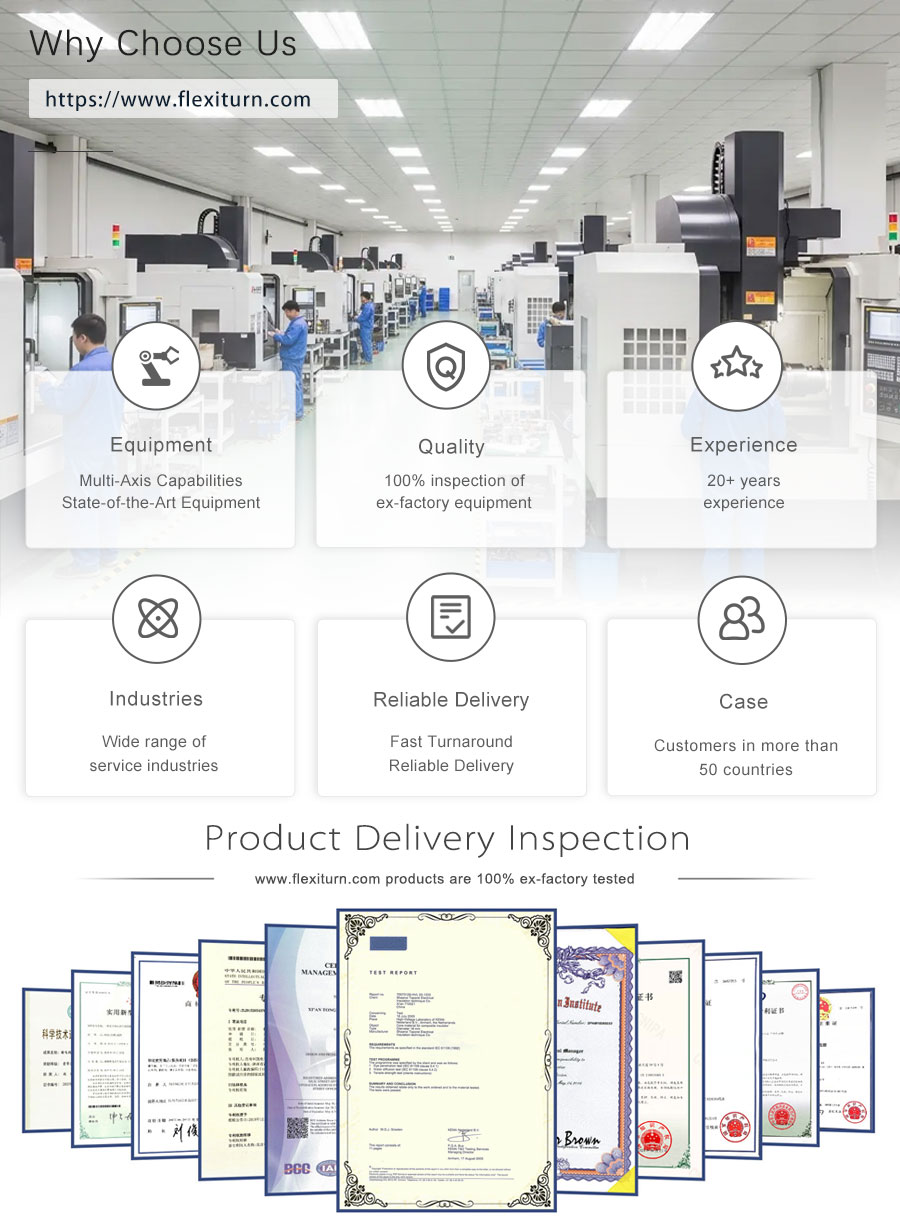
FlexiTurn performs in-process dimensional verification and final CMM inspection on critical features. Material certificates and dimensional reports are available upon request. The quality management system is ISO 9001:2015 certified.
Surface Finishing & Anodizing Compensation
Bare aluminum is not suitable for long-term service. FlexiTurn coordinates finishing matched to your environment:
Anodizing (Type II or Type III): Black, clear, or custom colors for corrosion resistance and wear resistance. Type III hard anodizing is available where wear resistance at the bore or pilot diameter is required.
Bead Blasting: Uniform matte finish and reduced surface glare.
Chromate Conversion Coating: Conductive alternative where anodizing is not permitted.
Anodizing changes part dimensions. Oxide growth closes bores and grows outer diameters. FlexiTurn compensates critical bore and pilot dimensions at the machining stage, and masks or controls coating on functional surfaces where required, so final fit is maintained after finishing.
Why Choose FlexiTurn
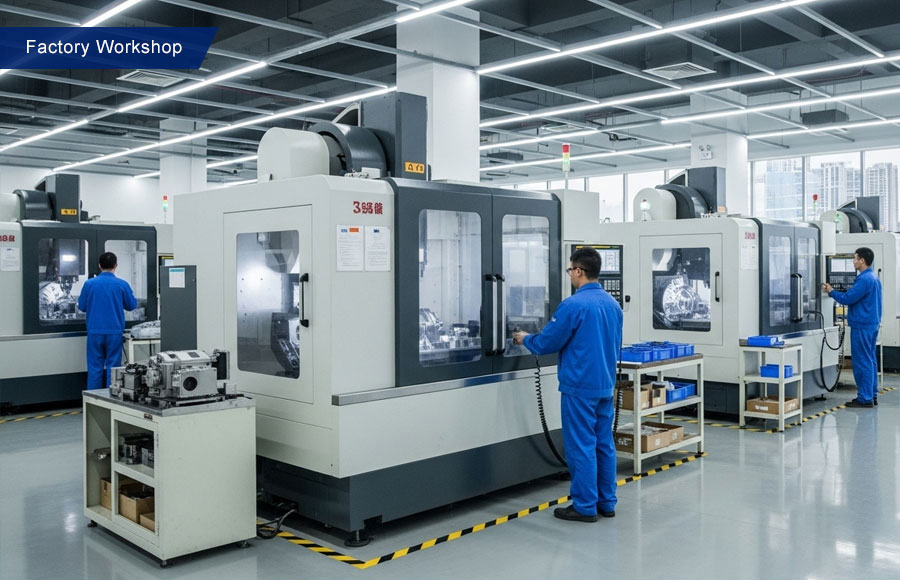
FlexiTurn is a China-based precision CNC machining service provider focused on custom engineered components.
- Unified-datum turning for rotational parts: Bore, pilot diameter, flange face, and outer diameter are machined relative to a common datum, reducing cumulative runout between locating and clamping features.
- Integrated turning and indexed milling: Stepped bores, pilot diameters, and bolt-hole patterns are machined with fewer re-fixturing steps.
- Anodizing-aware machining: We compensate critical dimensions before coating rather than discovering a fit problem after finishing.
- DFM review before production: We check bore accessibility, wall thickness, and tolerance stack-up against your drawing before quoting.
- Documented traceability: Certified raw materials and inspection reports with production orders.
FlexiTurn serves industries including automation machinery, robotics, industrial equipment, and non-implantable medical device subassemblies.
Get Started
Submit your 2D/3D CAD files, specify the aluminum grade, bore and pilot diameter tolerances, required surface finish, and anodizing requirement. FlexiTurn’s engineering team will review your flange design, provide DFM feedback, and deliver a detailed quotation.
Upload CAD Files for DFM Review
Contact FlexiTurn today to discuss your aluminum ring flange machining requirements.
FlexiTurn – Precision Machining, Delivered with Trust.
Q1. What types of machining services do you offer?
We provide comprehensive CNC turning and milling services. FlexiTurn machines are equipped with 8-station programmable turrets and support both turning and 5-axis milling operations, making them suitable for everything from simple cylindrical parts to complex multi-axis components.
Q2. What materials can you work with?
We machine a wide range of materials including carbon steel, stainless steel, aluminum, plastics, and other engineering-grade materials. If you have a specific material in mind, just send us your requirements and we'll confirm feasibility.
Q3. What is your typical lead time?
Lead times vary depending on part complexity, quantity, and material availability. For prototypes and small-batch runs, we typically deliver within 5–10 business days. For high-volume production, we'll provide a customized schedule after reviewing your drawings. Contact us with your project details for an accurate timeline.
Q4. How do you price your services?
Pricing is based on several factors: material cost, machining time, tooling requirements, setup complexity, and order quantity. We offer competitive rates for both low-volume prototypes and high-volume production runs. Request a quote with your CAD files or drawings and we'll get back to you within 24 hours.
Q5. What quality control measures do you have in place?
We follow strict quality control procedures throughout the machining process. Our CNC systems support programmable precision down to 1 μm, ensuring high accuracy and repeatability. Every batch undergoes dimensional inspection before shipping, and we can provide inspection reports upon request.