420 Stainless Steel Blanks
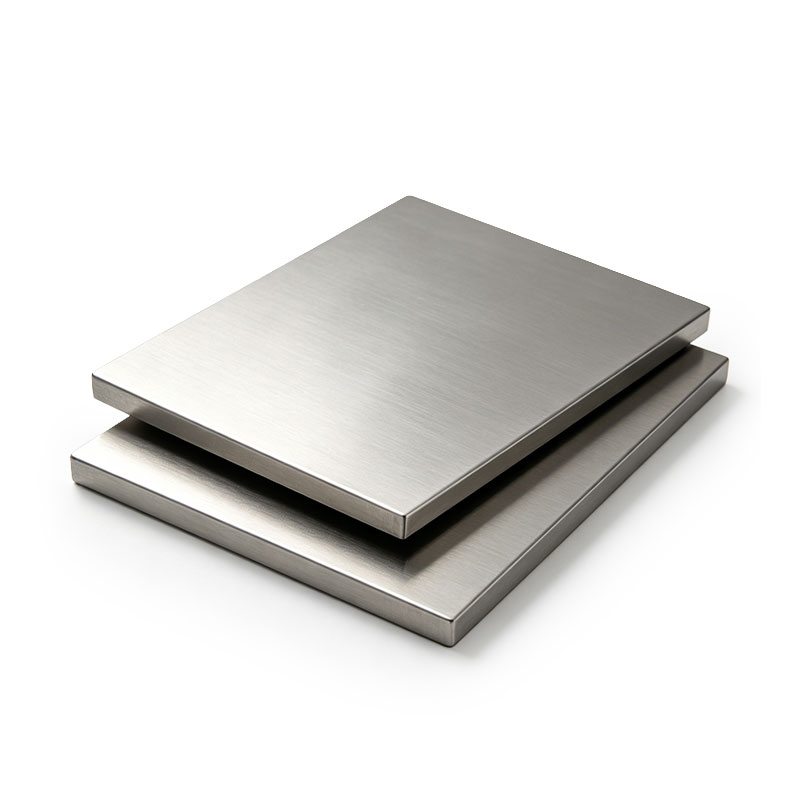
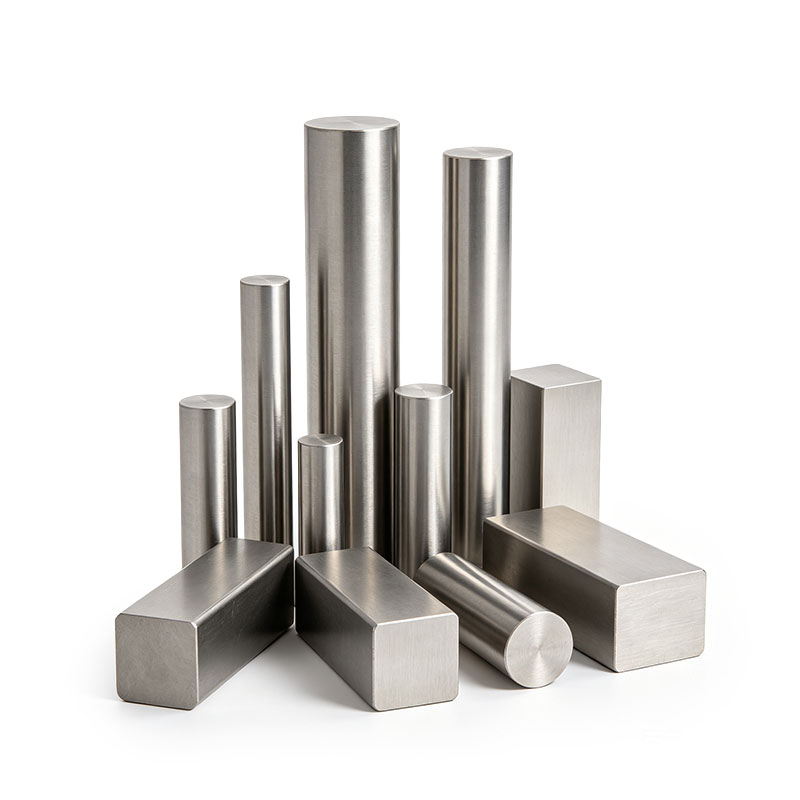
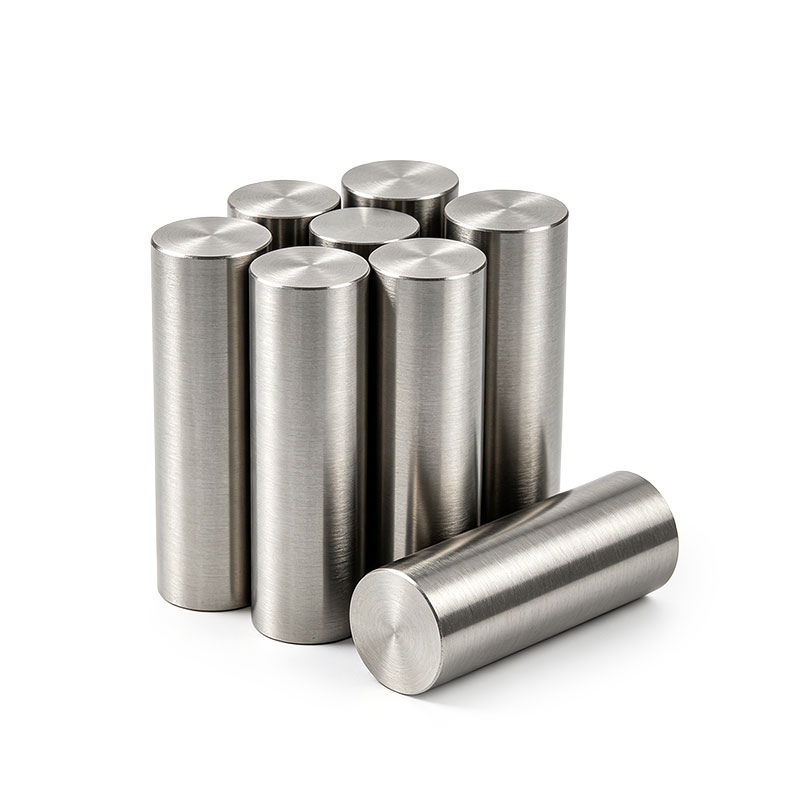
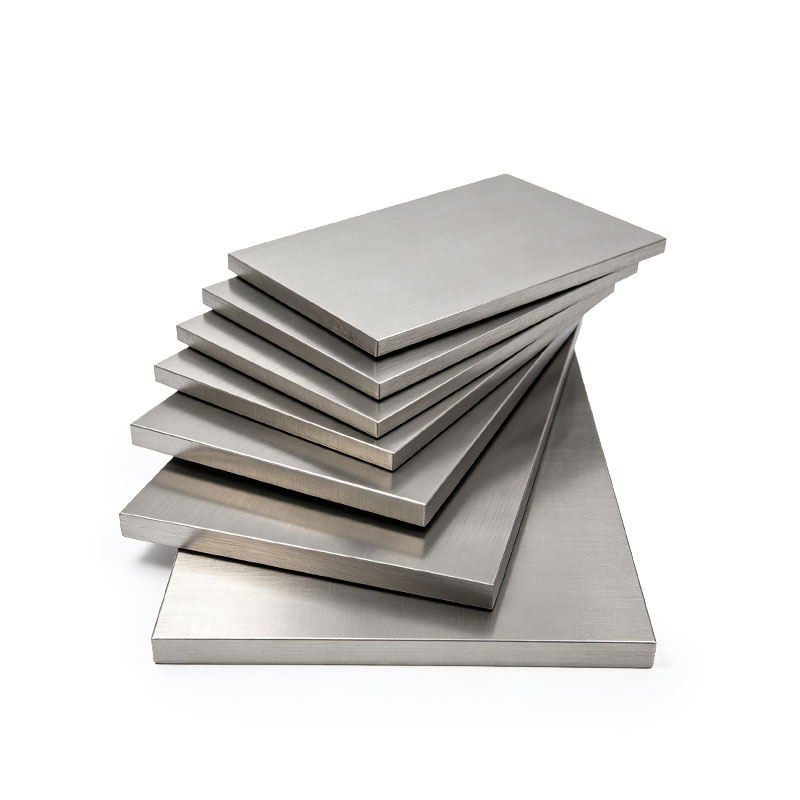
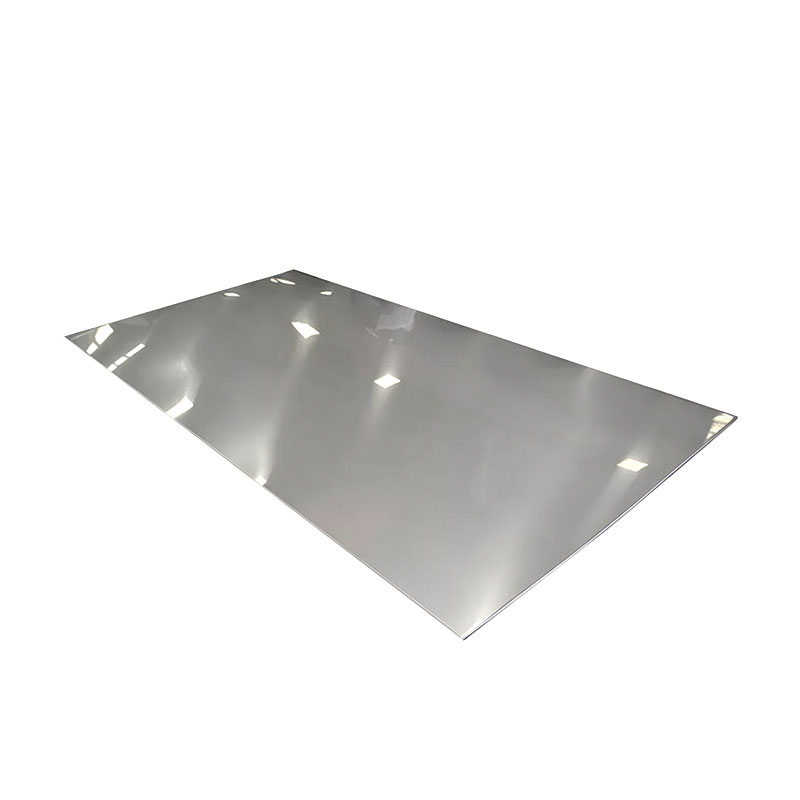
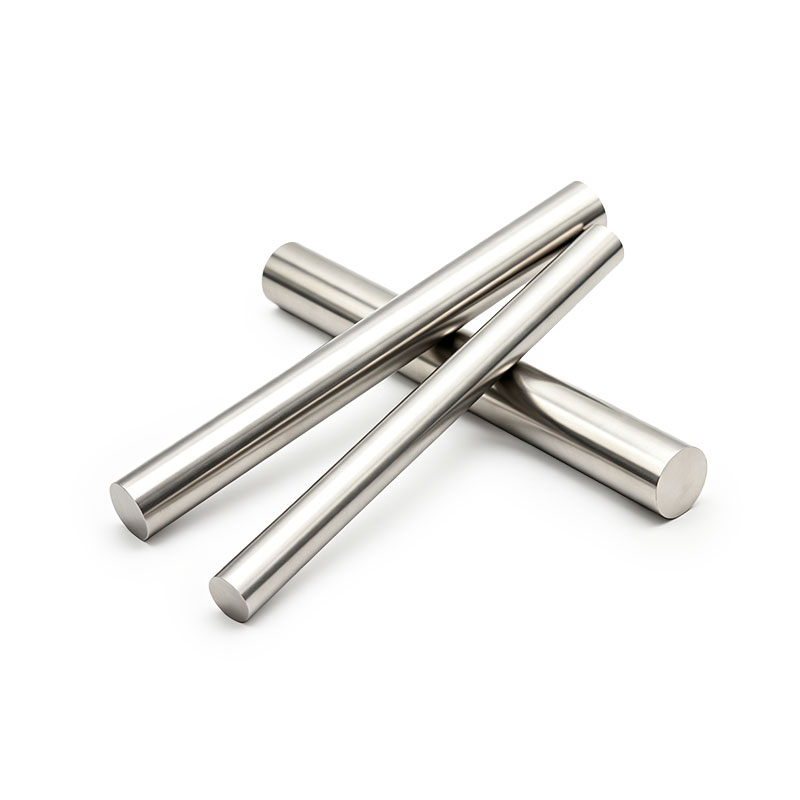
At FlexiTurn, we specialize in providing custom 420 Stainless Steel Blanks & Pre-Machining Services covering a full spectrum of product forms - including plates, round bars, tubes, and forged blocks across various supply conditions (Soft Annealed / Sphero-Annealed, or pre-quenched & tempered Q&T up to 50–55 HRC, covering 420J1, 420J2, and 420C variants) tailored to our customers' exact drawings and procurement specifications. Moving beyond traditional specialty steel suppliers who only sell full-length bars, heavy mill plates, or require high-volume mill orders, we offer a full suite of front-end pre-machining services: custom blank sizing, precision cut-to-length sawing (±0.1mm tolerance), cold NC waterjet/saw plate cutting, 6-side rough milling/squaring, inner/outer trepanning (preserving solid inner cores), pre-heat treatment (annealing/Q&T), and surface grinding or shot blasting.
420 Stainless Steel Blanks FAQs
What you may want to know about 420 Stainless Steel Blanks
420 Steel Raw Material Sourcing, Export Credentials & Heat-Lot Traceability
At FlexiTurn, resilient specialty steel supply chains, transparent traceability, and compliant export capabilities form the core of our 420 Stainless Steel Blanks service:
Compliant Sourcing from Primary Mills: We source exclusively from primary mills certified to ASTM A276, ASTM A473, or EN 10088-3 standards, strictly controlling carbon (C), chromium (Cr), and impurity ratios (P, S) to ensure uniform high hardness and wear-resistant microstructures post-quenching.
End-to-End Heat/Lot Number Tracking: From raw material intake, waterjet cutting, sawing, grinding, 6-side milling, and trepanning to heat treatment and final packaging, every individual blank or bundled unit is tagged with its original furnace heat and batch control numbers for 100% lot traceability.
Complete Certification & MTR Documentation: Every shipment includes an EN 10204 3.1 Mill Test Report documenting spectral chemical analysis, annealed hardness (HBW), and Q&T hardness (HRC) test results.
Rust-Proof & Heavy-Duty Export Packaging: All pre-machined 420 martensitic steel blanks undergo chemical washing and anti-rust oil application, isolated with moisture-proof plastic film. They are secured inside fumigation-free export wooden crates with heavy-duty reinforced padding to ensure zero rust and impact damage during transoceanic transit.
420 Steel Core Pre-Machining Services: Sawing, Waterjet Cutting, Heat Treatment & Trepanning
To meet the demands of high-hardness blades, mold inserts, and valve trim, FlexiTurn offers versatile pre-processing capabilities for 420 martensitic stainless steel:
Precision Sawing & Cold NC Waterjet Cutting: Utilizing heavy-duty CNC band saws and ultra-high-pressure waterjet cutting systems, we cut 420 forged bars and thick plates to exact customer dimensions. Cold waterjet processing generates zero Heat-Affected Zone (HAZ), preventing localized self-quenching hardening or edge cracking.
Pre-Heat Treatment Conditioning (Annealing & Quenching/Tempering): We supply blanks in Spheroidized Annealed state or pre-hardened/tempered to specified ranges like 30–35 HRC or 48–52 HRC per customer drawings, enabling clients to choose between soft rough machining or hard finish turning based on their in-house machine capabilities.
6-Side Milling & Surface Squaring: We perform 6-side rough milling and squaring on block-shaped mold, valve, or structural blanks, removing scale and decarburized layers while providing clean reference datums and tight perpendicularity.
Trepanning & Annular Core Cutting: For large-diameter solid bars or thick plate rings, dedicated trepanning tools slice out internal voids while saving the solid center core for reuse as smaller pins or bushings, dramatically reducing raw material waste on expensive high-hardness alloys.
Quality Control & Metallurgical Integrity in 420 Steel Pre-Machining
Because mechanical properties vary drastically between annealed and hardened states, high-carbon martensitic steel is susceptible to quenching cracks and surface decarburization, requiring strict process control:
Hardness & Metallurgical Inspection: Utilizing Brinell (HBW) and Rockwell (HRC) hardness testers, 100% sampling inspections are conducted on annealed or heat-treated batches to ensure hardness ranges comply strictly with ASTM / EN specifications.
Dimensional & Geometrical Inspection: Utilizing micrometers, calipers, and profilometers, final inspections are conducted on cut lengths, milling parallelism, and surface roughness before dispatch to leave optimal, uniform machining allowances for downstream CNC operations.
Ultrasonic Non-Destructive Testing (UT): For high-pressure valve, critical shaft, and mold insert blanks, ultrasonic testing per ASTM A388 is executed upon request to confirm zero internal shrink voids, flakes, or forging cracks.
420 Steel Client Value & Fulfillment Assurance
By choosing FlexiTurn's custom 420 stainless steel precision blanks and pre-machining services, overseas buyers gain distinct competitive edges:
Overcoming High MOQ & Large Bar Constraints: Avoid restrictive commitments for tonnage orders or full forged bars, purchasing exact pre-cut blank dimensions and quantities to optimize cash flow.
Avoiding Tool Wear & Thermal Cracking: Front-end 6-side milling and optimal condition selection minimize local CNC tool wear during hard cutting while eliminating the risk of part warping or cracking caused by post-machining quenching.
Seamless Customs Clearance & Compliance: With full export qualifications, authentic 3.1 MTRs, and industrial certifications, high-hardness martensitic alloy shipments clear customs smoothly while meeting destination country technical standards.
420 Steel Support & Contact Engineering Team
If you are seeking a reliable supplier with a resilient 420 martensitic stainless steel supply chain, full export credentials, and proven capabilities in precision blank waterjet cutting, 6-side milling, annealing/Q&T heat treatment, and trepanning, the FlexiTurn team is ready to assist.
Please send your required drawings (CAD/STEP), heat treat condition requirements (e.g., Annealed, 30–35 HRC, 50–55 HRC), blank dimensions, tolerances, and documentation needs (e.g., MTRs, hardness logs, UT reports) to our engineering sales team at: sales@flexiturn.com. Our technical team will respond within 24 hours with tailored pre-machining guidance and a detailed quotation.